
Who this machine is for
Every printer on the floor - and specifically for buyers who have been burning out the wrong resin and blaming the casting stage for it.
Jewellery 3D Printers & Resins · Resins
Five resins across two families - one that burns out in the flask, one that never should.
Request a quote
Pricing depends on configuration, quantity and your requirements.
DC & NC Resin Range
Jewellery 3D Printers & Resins
Overview
Every printer on the floor - and specifically for buyers who have been burning out the wrong resin and blaming the casting stage for it.
Specifications
5 parameters, as printed in our catalogue.
The range
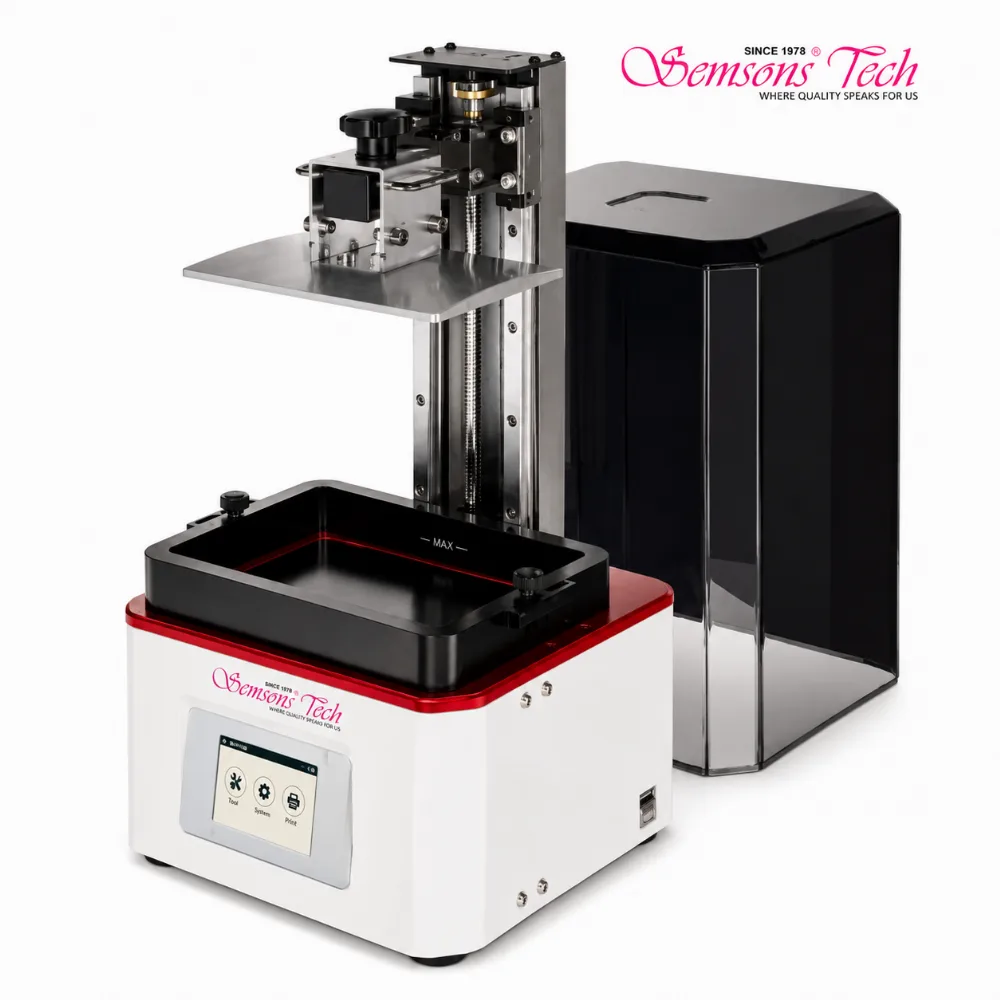
The larger-volume LCD printer - batch printing where build volume per rupee is what matters.
The highest-capacity LCD printer in the range - same build volume as the FOTO 6K, half again the daily output.
The compact DLP - a 10 um minimum layer in the smallest footprint of the S3D series.
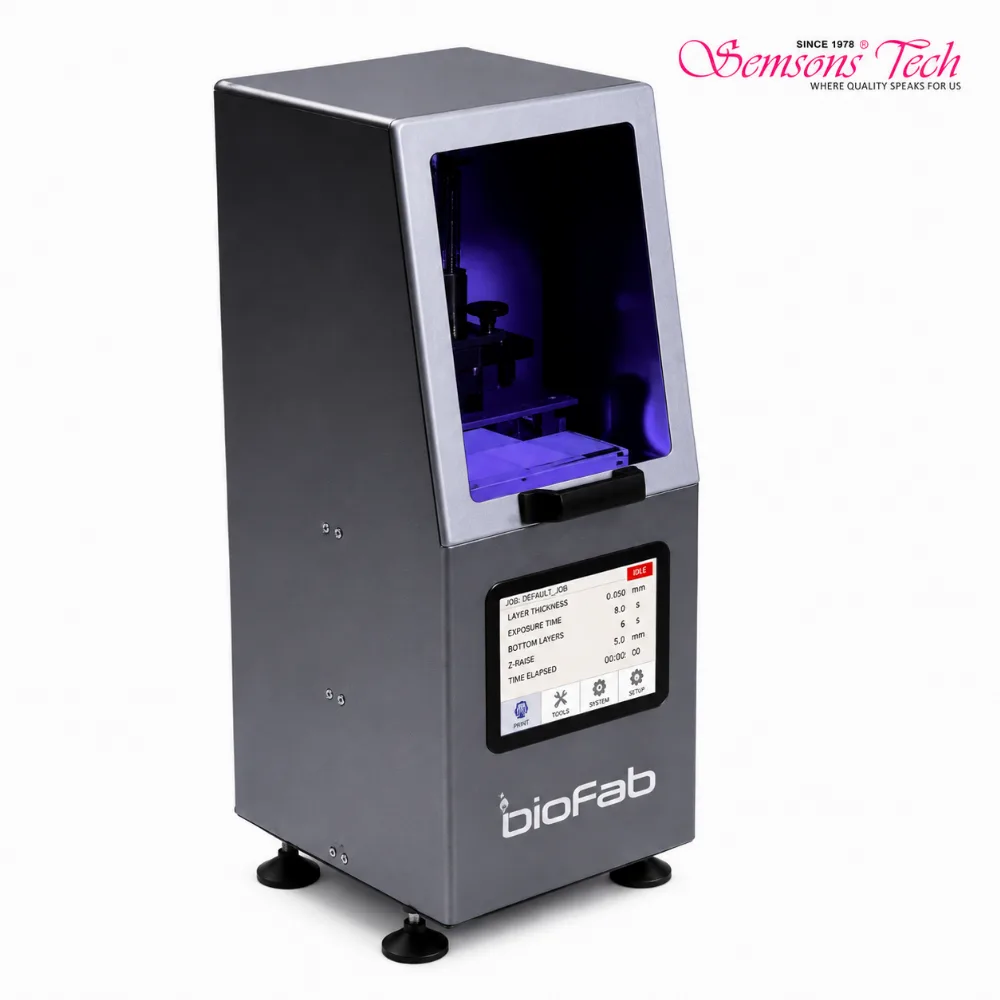
The finest XY resolution we publish - 49 um, for the most detail-critical work on the floor.
The largest plate in the DLP series - 192 x 108 mm with a 10 um minimum layer.
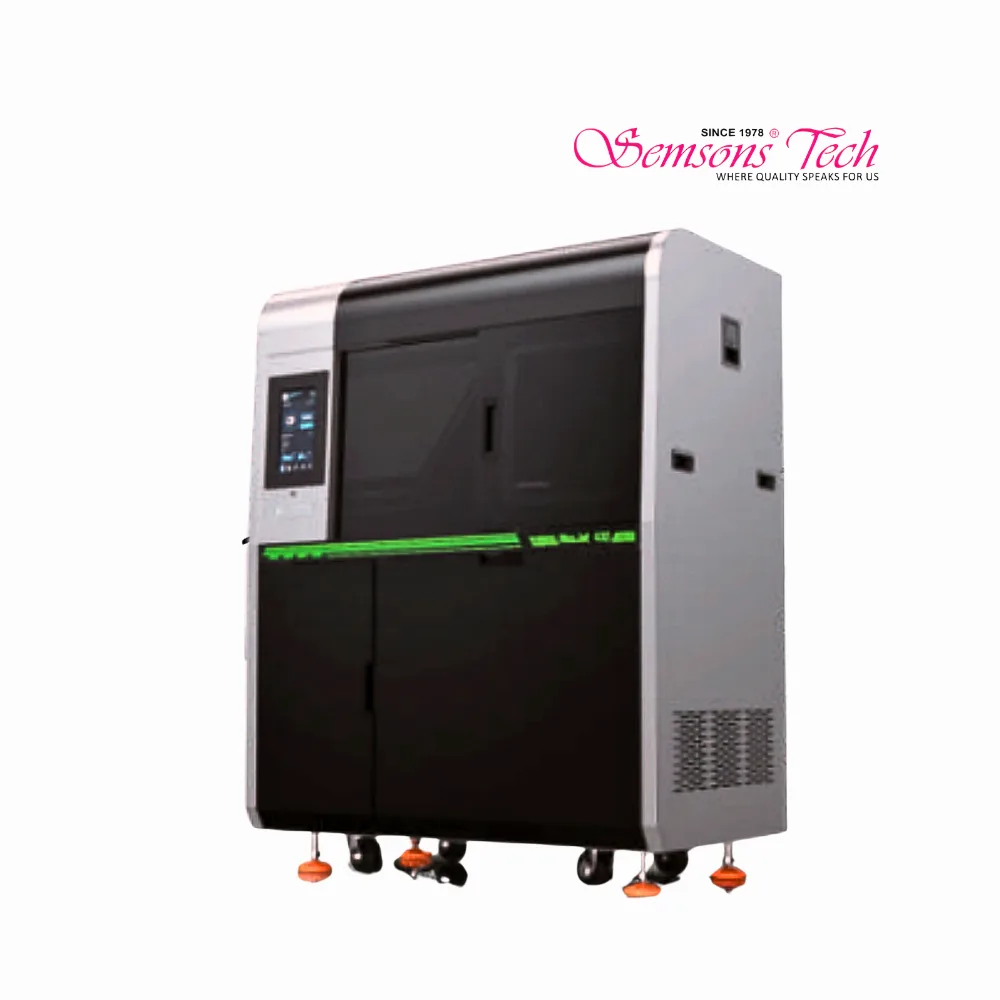
MJM wax jetting - the highest daily output and the tightest dimensional accuracy in the range.
Questions
Straight answers from the people who install and service these machines. Anything not covered here, ask us on the form below.
Direct-castable resin (our DC range) is formulated to burn out cleanly in investment, so the printed pattern goes straight into the flask like a wax. Non-castable resin (our NC range) is for fit checks, client approvals and master models that will be moulded rather than burned out. Printing an approval model in castable resin wastes money; casting a non-castable pattern ruins the flask - and usually the investment and the shift with it.
DC Yellow and DC Green are catalogue-specified for DLP at 405 nm. DC Black is listed as direct castable without a wavelength note. If you are running one of the S3D DLP machines, tell us which model and we will confirm the resin against it in writing rather than have you find out on a plate.
Because a non-castable model exists to be measured, fitted or moulded. If it bends after cure, every downstream decision made from it is wrong - the ring size, the stone seat, the rubber mould. That is the whole reason the property is called out separately in the catalogue.
Yes. We commission the machine on your floor and train your operators on your own material and your own designs rather than a demonstration sample. Semsons Tech has served the diamond and jewellery industry since 1978, and on our setting machines the control system is self-developed, so support does not depend on a third party abroad.
We do not publish delivery times, spare-parts pricing or AMC terms, because all three depend on configuration, destination and what is on the floor at the time. They are confirmed in writing on your quotation rather than estimated here. Ask for them explicitly when you enquire and you will get them in writing.
The DC & NC Resin Range is quoted to your configuration, quantity and delivery location. Send us your requirement through the form on this page, or message or call our sales team, and you will receive a written quotation.
Quotation
Tell us your designs, stone sizes and target output. We reply within one working day with the right configuration and a written quotation.
Your enquiry reaches our team tagged to this exact model, so you will not be sent a generic brochure.